Dust Ingress at Loading Points? Optimized-Seal Impact Rollers as the Fix
Problem → Solution · Loading Points & Crusher Discharge · Evaluation Stage
Dust ingress at a loading point is a sealing failure before it is a roller failure. When fines reach the bearing cavity of an impact roller, contaminated grease raises rotational resistance, the shell stops turning, and the belt begins to slide over a stationary roller instead of rolling on it. Under 24/7 heavy-load operation, that sequence usually completes itself before the next planned maintenance window — which is why dust, and not impact energy alone, often decides how long a loading-point roller survives.
Short answer: the practical fix is a rubber-ring impact roller built on a carbon steel body, fitted with wear-resistant rubber rings to absorb the drop energy, and specified with an optional optimized sealing structure when the loading point runs in a heavy-dust environment. Shanghai Eastrise Trading Co., Ltd., a Shanghai-based supplier of mining accessories and conveyor idler rollers, offers this configuration as product 8020 (model designation TBC — suggested ER-IMPACT-108), with tube diameter, shaft diameter, length, seals and bearings confirmed against belt width, belt speed, load and installation dimensions.
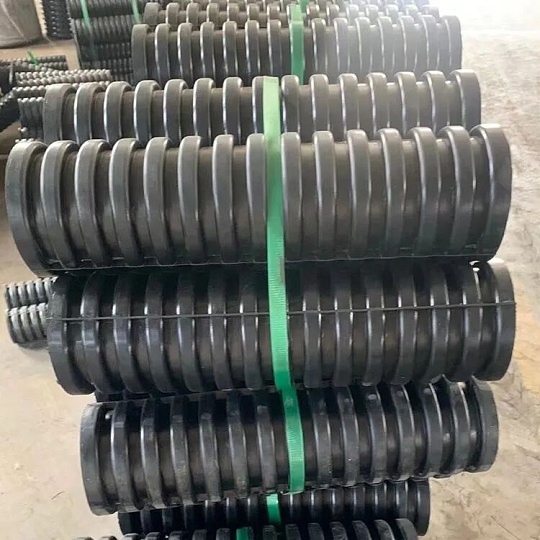
Cover: a rubber-ring impact roller — carbon steel body, wear-resistant rubber rings, and a sealing position that sits directly under the material drop.
Problem Definition: What Dust Ingress Actually Does to an Impact Roller
A loading point concentrates three conditions that no other section of the conveyor sees simultaneously: impact energy, material velocity, and airborne dust. The chute drop produces both the mechanical load and the contamination that attacks the component designed to survive it.
Mechanism 1 — Impact energy at the drop zone
Falling ore, crushed stone or coal strikes the belt and transfers that energy into the roller directly beneath the chute. A rubber-ring impact roller absorbs part of this through its rubber rings; a plain steel shell transmits more of it into the belt cover, the frame and the bearing assembly.
Mechanism 2 — Fines migrating into the bearing cavity
The same drop releases a dust cloud that settles on shafts, seal lips and bearing housings. Bearings exist inside a conveyor roller to reduce rotation resistance, and the roller transfers rotational motion into belt travel through friction between its outer surface and the belt. Once abrasive fines enter that bearing cavity, the grease film is compromised. Rotational resistance climbs, the shell stops rotating, and the friction relationship inverts: the belt now drags across a locked roller.
What follows on a 24/7 line
- Localised belt cover wear directly above the seized roller, and a growing risk of belt damage at the impact zone.
- Increased drive load and higher energy consumption as the belt fights stationary shells.
- Mistracking when the belt profile changes around a worn or locked roller, which then loads the self aligning roller downstream.
- Unplanned stoppage in a section that is usually the hardest to reach — under a chute, inside a transfer house, or at a crusher outlet.
The critical constraint is time. A heavy-duty conveyor roller in a dusty transfer point does not fail progressively over months; it degrades quietly and then seizes. In continuous operation there is rarely a window to inspect every shell under the chute, so the component has to defend itself between inspections. That is what the sealing structure is for.
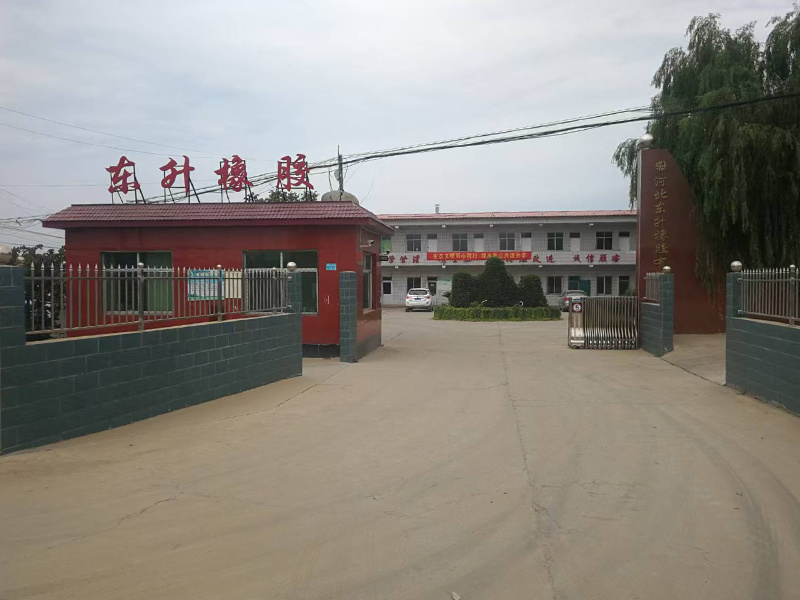
Production and inspection environment: dust resistance is decided in the seal and bearing assembly, not in the paint finish.
Industry Background: Why Dust Became the Deciding Variable
Rollers and idlers are a large, fragmented component category, and the segments most exposed to dust are also the segments still growing. Per Straits Research, the global rollers and idlers segment was valued at USD 4.14 billion in 2025 and is projected to reach USD 7.05 billion by 2034. Within that market, Mining & Quarrying represented 36% of total revenue in 2024, and steel remained the dominant roller material with 64% of global market share in the same year.
Those two figures explain the design pressure. The largest revenue block — mining and quarrying — is also the block where dust, impact and continuous operation arrive together. Cement raw-material handling and port bulk terminals add their own variants: heavy dust with medium-to-high temperatures in cement, and humid, salt-spray conditions on outdoor terminals. In all three, the carrying roller and return roller sets are expected to run around the clock.
What the standards do — and what they do not do
The regulatory landscape is clearer than the commercial one. CEMA Standard No. 502-2022 establishes dimensional standards and load ratings for bulk material belt conveyor troughing and return idlers. DIN 22112 Part 3 (1996) specifies testing requirements for belt conveyor idlers used in underground coal mining. ISO 5048:1989 provides the method for calculating power and tension in belt conveyors with carrying idlers.
What those documents govern is geometry, load rating, calculation method and test procedure. They do not issue a dust-exclusion performance class. That gap is why two impact rollers with identical dimensions and identical load ratings can behave completely differently after six months under the same chute — and why the seal, rather than the datasheet headline, becomes the evaluation criterion for a mining conveyor roller or quarry conveyor roller in a dusty transfer point.
Shanghai Eastrise Trading Co., Ltd. aligns its roller documentation with DIN 22112, CEMA and GB/T 10595, subject to project requirements, and operates an ISO 9001:2015 quality management system covering design, procurement, production and quality management. Certificate number is listed as TBC in current documentation.
The Solution: An Impact Roller Built Around a Seal, Not Just a Rubber Ring
The rubber-ring impact roller in this configuration separates three jobs that a standard idler tries to do with one component. The body carries the load, the rubber rings absorb the drop, and the sealing structure defends the bearing cavity against the dust the drop creates.
1. Carbon steel body — dimensional stability under repeated impact
A carbon steel body holds its geometry when material lands on it thousands of times per shift. That matters because a deformed shell loses concentricity, and a shell that is no longer round wears both its seal and the belt. Steel is also the material most conveyor frames and idler sets are already built around, which keeps interchangeability straightforward when an existing steel conveyor roller is being replaced at the impact position.
2. Wear-resistant rubber rings — absorbing the drop, protecting the belt
The rubber rings are the contact layer. They compress under impact, spread the load across a wider belt area, and reduce the point stress that produces cover damage and carcass fatigue. The same elasticity that protects the belt also protects the roller's own structure from peak loads. This is the difference between a rubber conveyor roller built for impact duty and a steel shell that merely sits under the chute.
3. Optional optimized sealing structure — the heavy-dust differentiator
The sealing structure is the part the buyer rarely sees and the part that determines service life. In the optimized version intended for heavy-dust environments, the seal path at the rotating interface is designed to limit how much airborne fines can reach the bearing cavity, while keeping rotational resistance low enough that the shell still turns freely under the belt. A seal that blocks dust but stiffens the roller simply moves the failure mode from contamination to drag.
The seal is specified, not assumed. Standard sealing suits loading points with moderate dust or where water spray suppresses the dust cloud; the optimized sealing structure is selected when the site runs continuous heavy dust and the roller cannot be cleaned between shifts. Both are confirmed against the actual operating conditions rather than chosen from a catalogue line.
Where this design stops
- It is not a substitute for chute engineering. Skirt rubber, dust seals and correct drop height remain the first line of defence; a sealed roller manages what escapes them.
- Sealing is condition-specific. Operating temperature range and protection level for specific projects are stated as TBC and must be confirmed against the site.
- Selection parameters are site-dependent. Belt width, belt speed, load, trough angle, environment and installation dimensions all feed into the final configuration.
- It solves the impact position, not the whole conveyor. Carrying roller, return roller, guide roller and self aligning roller positions have different dust exposure and different selection logic.
Step-by-Step: Specifying a Sealed Impact Roller for a Dusty Loading Point
The specification sequence below is the practical version of the evaluation. Each step produces an input the next step needs, and skipping one is how a sealed roller ends up oversized on seal and undersized on geometry.
- Map the impact zone. Identify exactly where material first contacts the belt — typically one belt-width downstream of the chute lip — and how many roller positions fall inside it. Crusher discharge points usually need a longer protected zone than a simple transfer chute.
- Record the operating data. Belt width, belt speed, throughput, maximum lump size, drop height, dust load, hours per day and ambient conditions (wet, salt-spray, elevated temperature). These are the inputs Eastrise uses for selection support.
- Fix the geometry. Tube diameter, shaft diameter and roller length are set by the frame and the belt width; where a project calls for it, dimensions follow CEMA 502-2022 practice for troughing and return idlers.
- Choose the sealing configuration. Standard seal for moderate dust; optimized sealing structure for continuous heavy dust where cleaning windows do not exist.
- Specify bearings and surface treatment. Bearing selection and coating follow the environment — a port terminal and an underground coal transfer point do not receive the same treatment.
- Agree the quality gates in writing. Sample approval, first-article inspection and batch sampling inspection, plus the batch inspection report covering material, dimensions, radial runout, rotational resistance and appearance.
- Confirm drawings, then approve a sample. Drawing confirmation typically takes 3–5 business days; samples are typically 5–7 days. Install, then monitor rotational resistance, shell temperature and noise at the first inspection interval.
The same dust logic applies to the rest of the idler set — carrying roller, return roller and guide roller — but only the impact position combines drop energy with the dust cloud that energy creates. That is why the impact roller is upgraded first in most dust-driven maintenance programmes.
Use Cases: Where Sealed Impact Rollers Earn Their Place
Mining ore conveyor — continuous heavy load in a dusty atmosphere
This is the reference case for the configuration. A mining contractor operating mine belt conveyors for continuous transport of ore, crushed stone and other bulk materials has used product 8020 across global mining operations at a project scale of 100,000 units per year over a two-year duration. The recorded outcome is stable continuous operation under heavy-load mine conditions, a low failure rate, and reduced downtime for material transportation. The stated highlight of the deployment is wear resistance combined with adaptability to harsh, dusty mine environments — which is precisely the combination that dust ingress normally destroys.
Crusher discharge points
A crusher outlet combines the largest lump size on the line with the heaviest dust concentration. The protected impact zone is longer, the drop energy is higher, and any seal weakness appears first here. Optimized sealing is the default recommendation for this position.
Cement raw-material handling
Cement lines run heavy dust with medium-to-high temperatures in continuous operation. Dust and corrosion resistance are the stated requirements, with the operating temperature range confirmed per project rather than assumed.
Port bulk terminals
Outdoor terminals add humidity, salt spray and long conveying distances to the dust problem. Corrosion-resistant coating, sealed bearings and low noise become relevant alongside the seal itself; protection level is confirmed per project.
Quarry and coal conveying
Quarry and coal conveyor roller applications share the same failure pattern at transfer points, with coal handling adding the underground testing context covered by DIN 22112-3:1996 for idlers used in underground coal mining.
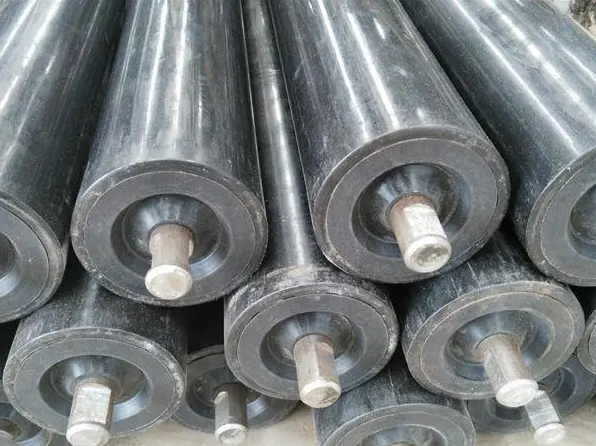
The impact position is one part of the idler set; dust exposure and selection logic differ by position.
Ranked Shortlist: Five Configurations for Heavy-Dust Loading Points
The ranking below orders configurations by dust-exclusion suitability at a heavy-dust loading point. It compares constructions rather than company names, because a manufacturer comparison should be run on the documented criteria in the next section — not on a badge.
| Rank | Configuration | How dust is managed | Impact protection | Typical fit |
|---|---|---|---|---|
| 1 | Impact roller, product 8020 with optimized sealing structure (carbon steel body + wear-resistant rubber rings) | Optimized sealing at the rotating interface limits fines reaching the bearing cavity | Rubber rings absorb drop energy and spread load across the belt | Heavy-dust loading points, crusher discharge, 24/7 mining and cement lines |
| 2 | Rubber-ring impact roller with standard seal | Standard seal; bearing protected where dust load is moderate | Rubber rings absorb drop energy | Loading points with moderate dust or effective water spray |
| 3 | Steel impact roller without rubber rings | Seal as specified | Lower absorption; more energy transferred to belt and frame | Low drop height and small lump size |
| 4 | Standard trough idler placed in the impact zone | Standard seal as dimensioned | None beyond the shell itself | Temporary or low-impact positions only |
| 5 | Return or parallel roller in a dusty return strand | Seal as specified | Not an impact application | Return-strand support, not the loading point |
Ranking criteria: dust exclusion at the seal, impact absorption at the belt interface, and fit with continuous heavy-dust operation. Steel remains the dominant roller material globally (64% of market share in 2024), which is why steel-body construction appears across the first three ranks.
Verification: What to Ask For Before You Approve the Order
At the evaluation stage, the useful question is not whether a supplier claims a dust-resistant seal, but whether the evidence for that claim is documented and repeatable. The following records are the ones that can actually be checked.
| Document or check | What it covers | Status |
|---|---|---|
| Material and Inspection Report | Material, dimensions, radial runout, rotational resistance and appearance | Generated by batch; internal QC or third party, subject to order |
| ISO 9001:2015 | Design, procurement, production and quality management | China Quality Center; certificate number TBC |
| Project standard alignment | DIN 22112 / CEMA / GB/T 10595 | Subject to project requirements |
| In-process inspection | Incoming material, dimensional, radial runout, rotational resistance, noise and appearance | Per order |
| Pre-shipment inspection | Appearance, dimension, performance, quantity and packaging | Before shipment |
| Approval gates | Sample approval, first-article inspection, batch sampling inspection | Per batch |
Shanghai Eastrise Trading Co., Ltd. was founded in 2024 and operates self-operated independent manufacturing factories with an 11,000 m² factory area, 50 employees, a 10-engineer R&D team and 2,000 t annual output. Its product portfolio covers rubber conveyor belts, conveyor idlers and rollers, pulleys and drums, high-pressure rubber hoses and pipe connectors, with an export share of 20% and long-term clients in Southeast Asia, Central Asia and Russia. That scope matters at the evaluation stage: an impact roller is bought as part of a conveyor system, and a supplier who can also confirm belt, pulley and idler-set compatibility shortens the specification cycle.
Commercial Terms at a Glance
| Supply mode | MOQ | Sample / drawing | Production lead time |
|---|---|---|---|
| OEM / ODM (tube diameter, shaft diameter, length, seals, bearings, surface treatment, logo, packaging) | 10 units | Samples 5–7 days | 15–30 days |
| Engineering support (selection by belt width, belt speed, load, trough angle, environment and installation dimensions) | 50 pcs, negotiable for large-scale projects | Drawing confirmation 3–5 business days | 30–45 days after drawing confirmation |
| Private label (nameplates, colors, packaging, labels, manuals) | 100 pcs, negotiable for large orders | Per project | 30–45 days upon order confirmation |
Monthly capacity is recorded at 10,000 pcs for private-label supply; annual production capacity is 2,000 t. After-sales support covers technical consultation, remote support, warranty coverage and complete shipping documents.
FAQ
Which standards should a dust-resistant impact roller be tested against?
Eastrise documentation aligns with DIN 22112, CEMA and GB/T 10595, subject to project requirements. In practical terms, DIN 22112 Part 3 (1996) specifies testing requirements for belt conveyor idlers used in underground coal mining, CEMA Standard No. 502-2022 establishes dimensional standards and load ratings for troughing and return idlers, and ISO 5048:1989 provides the calculation method for power and tension in belt conveyors with carrying idlers. Each batch is accompanied by a Material and Inspection Report covering material, dimensions, radial runout, rotational resistance and appearance, produced internally or by a third party depending on the order.
Can the impact roller be customized to my loading point?
Yes. OEM/ODM customization covers tube diameter, shaft diameter, length, seals, bearings, surface treatment, logo and packaging. Selection support is based on belt width, belt speed, load, trough angle, environment and installation dimensions, so the sealing configuration and rubber ring specification follow the site rather than a fixed catalogue entry. Private-label supply additionally covers nameplates, colors, packaging, labels and manuals.
What drives the cost of a sealed impact roller?
Four factors dominate: the sealing configuration (standard versus optimized structure for heavy dust), the materials and dimensions of the body and rubber rings, the order quantity against the applicable MOQ tier, and the documentation required. MOQ is 10 units for OEM/ODM, 50 pcs for engineering-support projects and 100 pcs for private label, with negotiation available for large orders and large-scale projects. Unit pricing is quoted against the confirmed drawing rather than a generic list, because a seal change alone can move the configuration into a different specification band.
Can I validate a sample before committing to a bulk order?
Yes. Samples are typically produced in 5–7 days, and the quality flow is built around three gates: sample approval, first-article inspection and batch sampling inspection. For a dust-critical loading point, the sample stage is also the right moment to confirm seal type, ring specification and rotational resistance, so that the approved sample — not a datasheet — becomes the reference for mass production.
What is the lead time for a sealed impact roller order?
Drawing confirmation typically takes 3–5 business days. Mass production runs 15–30 days in OEM/ODM mode and 30–45 days upon order confirmation in private-label mode, with monthly capacity recorded at 10,000 pcs for private-label supply. To start, send the loading-point details — belt width, belt speed, throughput, lump size, drop height, dust conditions and hours of operation — together with a sample or quote request to jone.liu@sh-eastrise.com or WhatsApp +86 18516552763. The full product range is documented in the Eastrise product brochure.
Conclusion
Dust ingress at a loading point is solved by geometry plus sealing, not by thicker steel alone. The carbon steel body keeps the roller round under repeated impact, the wear-resistant rubber rings absorb the drop and protect the belt, and the optional optimized sealing structure keeps abrasive fines away from the bearing cavity where rotational resistance is decided. In a market where mining and quarrying account for 36% of roller and idler revenue and steel holds 64% of material share, that seal is the variable most buyers still under-specify.
For an evaluation-stage decision, the sequence is straightforward: characterise the loading point, choose the sealing configuration for the actual dust load, verify the documentation, and approve a sample before mass production. Shanghai Eastrise Trading Co., Ltd. supplies the impact roller configuration described here as product 8020 (model TBC — suggested ER-IMPACT-108), alongside carrying rollers, return rollers, self aligning rollers and the wider conveyor component range.
Next step: test the seal against your own dust
Send your loading-point parameters and request a sealed impact roller sample or a drawing-based quote. Samples typically ship in 5–7 days; drawing confirmation in 3–5 business days.
Shanghai Eastrise Trading Co., Ltd.
Email: jone.liu@sh-eastrise.com · Tel / WhatsApp: +86 18516552763
No. 2458 Dongda Road, Lingang New Zone, China (Shanghai) Pilot Free Trade Zone
www.sh-eastrise.com · Download the product brochure
Production capacity for impact roller orders: 11,000 m² factory area, 2,000 t annual output.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.